How Is Copper Extracted from Ore? Mine to Concentrate
A mine owner's plain-language route from mine to concentrate, covering sulphide flotation and oxide leaching.
Say a mine owner asks, on a dusty walk around a drill site, how is copper extracted from ore. You don't answer with a single flow sheet. You answer with a route decision. Copper extraction splits early. The split depends on the ore minerals in front of you. Sulphide ore goes one way. Oxide ore goes another. Sometimes the two need a mixed circuit.
Copper ore types: what determines the extraction route
Not all copper ore is the same mineral. Most copper on earth sits in sulphide minerals: chalcopyrite, bornite, chalcocite. Near the surface, oxygen and water attack those sulphides. That produces oxide minerals: malachite, azurite, cuprite, tenorite. Oxide ores are usually lower grade. But they leach readily in dilute sulphuric acid. Sulphide ores are often higher grade. They resist leaching and respond better to flotation.
The first test isn't a single copper assay. It's a mineralogical study. Plain and simple. You need the oxidation ratio. Also the acid-soluble copper percentage. And a good look at the gangue minerals. Carbonate gangue, for example, will consume acid. It can kill an oxide leach. Iron sulphides change flotation behaviour. A mixed ore, part oxide and part sulphide, can demand a split circuit. Don't ignore that. According to Xinhai's published project data, a 1,000 t/d Bolivia mixed oxide-copper project had an oxidation ratio of 71.92% and copper recovery of 81.45%. That kind of ratio is a warning. Don't design a pure flotation plant for it.
The scale matters too. In 2024, U.S. mine production of recoverable copper was an estimated 1.1 million tons, down 3% from 2023, according to the USGS Mineral Commodity Summaries 2025.
| Attribute | Sulphide ore | Oxide ore |
|---|---|---|
| Common minerals | Chalcopyrite, bornite, chalcocite | Malachite, azurite, cuprite, tenorite |
| Preferred route | Froth flotation | Heap leaching plus SX-EW |
| Main product | Copper concentrate | Copper cathode |
| Key risk | Grade-recovery trade-off, penalty elements | Acid consumption, permeability, low recovery on refractory oxides |
| Decision driver | Mineralogy and liberation size | Acid-soluble copper and gangue carbonate content |
Mining the ore: open-pit and underground methods
Mining method is chosen long before processing. Near-surface deposits favour open pits. You dig stepped benches, drill and blast, and move ore in large haul trucks. It's lower cost per tonne for large, low-grade deposits. Simple economics. Underground mining uses shafts, tunnels, and methods like room-and-pillar or cut-and-fill. It disturbs less surface and suits deeper, narrower deposits. But it costs more and demands more ground control.
Strip ratio decides open-pit economics. It's the volume of waste moved per tonne of ore. That's the driver. A low strip ratio makes a low-grade open pit viable. A high strip ratio pushes you underground. Or it kills the project. Underground methods are selected by the shape and rock mass. Sub-level stoping suits steep, strong ore bodies. Room-and-pillar suits flat, tabular deposits. Match the method to the rock. Each method leaves a different dilution and recovery signature. That changes the grade arriving at the plant.
For a new copper project, don't wait for a mining study to think about grade variability. Blending matters. Feed a plant high sulphide ore one week and oxide ore the next. It'll struggle. The mining schedule and the process route must talk to each other early. No silos. For an overview of the full flowsheet, see the copper solutions page.
Crushing and grinding: liberating copper minerals
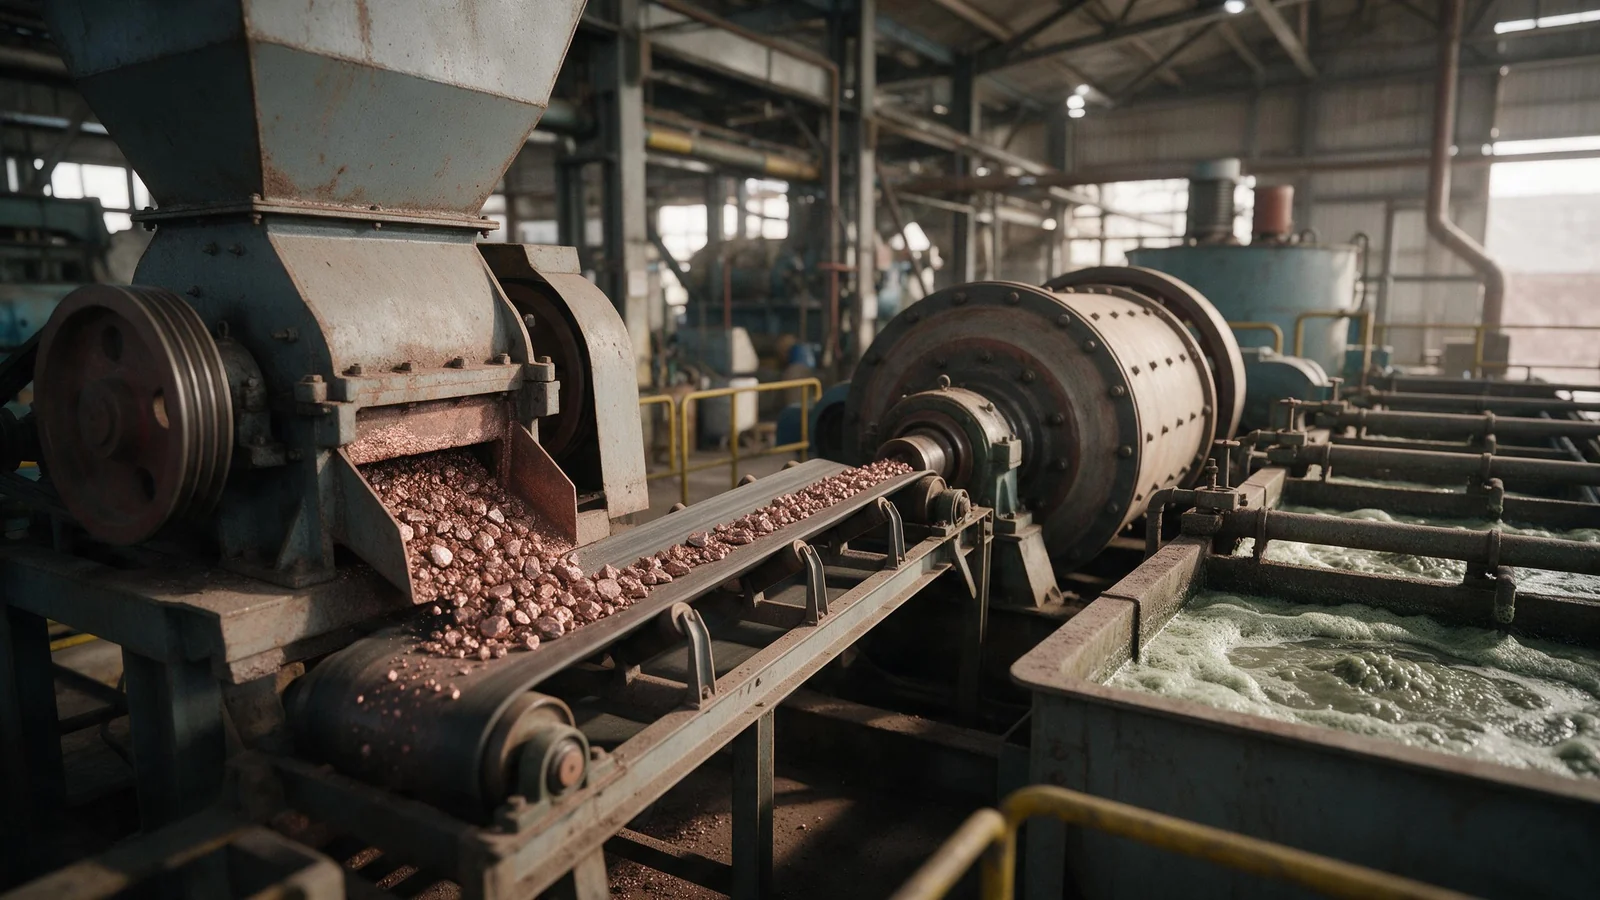
Once ore reaches the plant, it doesn't go straight to the flotation cell. It's blasted rock. Sometimes too big for a truck box. Primary crushing takes boulder-sized ore down to something like golf-ball size. A jaw or gyratory crusher does this near the pit or plant. Then ball mills grind it much finer. The goal: free copper minerals from waste rock.
For small-to-mid copper plants, the common circuit is two-stage crushing and one- or two-stage closed-circuit grinding. The target isn't a guess. It's set by a grindability test and a mineral liberation study. Testwork rules. P80 is the size 80 per cent of the mass passes. A typical copper flotation feed might have a P80 between 75 and 150 micrometres, depending on the ore. According to Xinhai's published project data, a Nigeria 1,000 t/d copper-silver plant used two-stage semi-closed crushing and two-stage closed-circuit grinding, from 68% to 90% passing 200 mesh. That means the final grind was fine enough to unlock copper minerals. Without overgrinding the gangue.
Closed-circuit grinding is the difference between a good plant and a bad one. Don't skip it. A classifier or cyclone returns the oversize to the mill. That keeps the mill from grinding already fine material. It prevents overgrinding, which wastes energy and creates slimes. Mill size is not chosen from a catalogue. It comes from a Bond work index test. That test measures the energy needed to break your ore. Not someone else's ore.
If you're working on a plant below 2,000 tonnes per day, the small-scale copper processing plant page goes through the equipment choices.
Sulphide ore: froth flotation to copper concentrate
For sulphide ore, flotation is the workhorse. You mix the ground ore with water and reagents. That's the start. Air bubbles carry copper minerals to the top of the cell as a froth. Scrape that froth off. That's your copper concentrate. The waste rock stays behind as tailings. Simple in concept.
Flotation isn't one cell. It's a bank of cells arranged as roughing, cleaning and scavenging. Roughing pulls out most of the copper quickly. Cleaning upgrades the rougher concentrate. It rejects more gangue. Scavenging catches the slow-floating copper that would otherwise go to tailings. Circuit design depends on the ore's flotation kinetics. That's why a locked-cycle test matters.
Concentrate grade and recovery are not free. Chase a higher grade and you might lose recovery. Push recovery and the grade drops. Testwork and economics settle the trade-off. According to Xinhai's published project data, a 1,500 t/d Pakistan sulphide copper project with 0.80% Cu feed produced a 20.78% Cu concentrate at 90.05% recovery. That's a clean, high-recovery result on a very low-grade feed. It didn't happen by luck. A locked-cycle flotation test and a conservative reagent regime did it.
For a mine owner, the key question isn't what grade can I make. It's what grade and recovery combination maximises payable copper minus costs. Ask the lab for a grade-recovery curve. That's your decision tool.
Oxide ore: heap leaching, solvent extraction and electrowinning
Oxide ore takes a different road. Crush it, stack it on an impermeable pad, and irrigate with dilute sulphuric acid. The acid dissolves copper from the rock. You get a pregnant leach solution. That's the feed to SX. That solution goes to solvent extraction. An organic extractant selectively pulls copper out of the weak, impure solution. Then you strip it into a strong, clean electrolyte. Electrowinning plates copper onto cathodes. Purity: 99.99 per cent.
Heap leaching suits low-grade, permeable oxide ore. Agitated leaching stirs crushed ore in tanks. It suits finer ore or higher grades but costs more in power and solid-liquid separation. The choice is still testwork. Run bottle roll tests and column leach tests before you commit. Acid consumption is measured in kilograms of acid per tonne of ore. That number often decides the project.
Leaching sounds simpler than flotation. It's not always cheaper. Acid consumption is the silent killer. Carbonate gangue can eat acid faster than it dissolves copper. Watch out. Poor permeability stalls the leach. Low percolation means you waste months. Time is money. Heap leaching works when the ore is acid-soluble, acid consumption is manageable, and the owner wants cathode rather than concentrate. All three must line up. For many oxide and mixed ores, a hybrid route is the right engineering answer. Leach the oxides, float the sulphides.
Smelting and refining: from concentrate to cathode
Once you have a concentrate, the mine owner's job usually stops. Smelting and refining belong to smelters. Not your problem. Sell the concentrate, or toll-treat it. The smelter mixes your concentrate with flux and heats it to around 1,230 to 1,300 degrees Celsius. That produces a molten copper-iron-sulphide matte. Converting blows air through the matte to remove iron and sulphur. That leaves blister copper at about 98.5 to 99.5 per cent copper. Electrolytic refining then produces 99.99 per cent copper cathode. That's the good stuff.
This step is outside the mine gate. But the concentrate quality you send still matters. Penalties for arsenic, mercury, bismuth and other impurities can destroy your payable copper. Read the smelter contract. A good flowsheet designs impurities out at the flotation stage. Not at the smelter.
Producing cathode from oxide ore via SX-EW? You skip smelting and refining entirely. The tankhouse cathode is already saleable.
What a mine owner should prepare before process design
Process design doesn't start with a CAD drawing. It starts with samples and questions. Ask the right ones. Before you approach a contractor or an EPC team, have a plan. Don't wing it.
- Representative samples from each ore zone, not a single grab sample.
- Full multi-element analysis plus copper phase analysis, including acid-soluble copper and oxidation ratio.
- Grindability and abrasion indices, plus any existing testwork reports.
- Target throughput, site conditions, power and water availability, and product preference: concentrate or cathode.
Don't guess the throughput. For small-to-mid copper plants, the typical range is 200 to 2,000 tonnes per day. The most common bracket is 300 to 1,500 tonnes per day. Smaller deposit? Modular plants work. Larger? The flowsheet changes. The plant size isn't a label. It's derived from your mine plan and ore reserve.
Timing matters too. A 500 to 1,500 tonnes per day flotation EPC typically takes 12 to 18 months from design to production. Plan for it. That's from the industry reference. Not a promise. Brownfield sites with power and permits ready can be faster. Remote greenfield sites will be slower. No surprise. Ask any contractor for a staged delivery: testwork first, then design, then equipment and construction. That reduces your risk. Big time.
Contractor says they have experience? Ask to see it. Ask for a process flow diagram from a similar ore. Also a test report with a grade-recovery curve. And the name of a reference plant you can call, with the owner's permission. Don't accept a brochure with no data. A serious engineering team will welcome these questions. They keep both sides aligned before money is spent.
And before you lock a reserve, get a mineral resource and ore reserve statement prepared under the JORC Code. It sets minimum standards for public reporting. That's the baseline. At the same time, look at the copper processing plant cost page for capital and operating structure, but remember no prices here.
Frequently asked questions
How is copper extracted from ore step by step?
First the ore is mined. Open pit or underground. Then it's crushed and ground. That liberates copper minerals. Sulphide ore goes to froth flotation. You get a copper concentrate. Oxide ore is heap leached with dilute sulphuric acid. The pregnant solution goes through solvent extraction and electrowinning. Result: copper cathode. Concentrate is later smelted and refined. That's the smelter's job.
How many years of copper are left in the world?
There is no fixed number you can trust without a dated reserve statement. The idea of years remaining is simply known reserves divided by annual production. It's a moving target. Both numbers change every year. Exploration adds reserves. Consumption rises or falls. Recycling also extends supply. Don't forget that. Before relying on any figure, ask for a mineral resource and ore reserve statement. It should be under the JORC Code or NI 43-101.
Why is copper mining so bad for the environment?
It's not automatically bad. But it creates serious risks if poorly managed. Waste rock and tailings can generate acid mine drainage. That happens if sulphides oxidise. Leaching uses acid. That acid must be contained. Mining also disturbs land, uses energy and water, and can affect local communities. All real impacts. Modern operations reduce these impacts. They use engineered tailings storage, water treatment, dust control and progressive rehabilitation. Ask any operator for their environmental management plan. Then judge.
What is copper ore?
Copper ore is rock that contains copper minerals. The grade must be high enough to mine and process economically. The main copper minerals are sulphides like chalcopyrite, bornite and chalcocite. Oxides include malachite, azurite, cuprite and tenorite. What counts as ore changes with copper price, mining cost and process technology. It's dynamic.