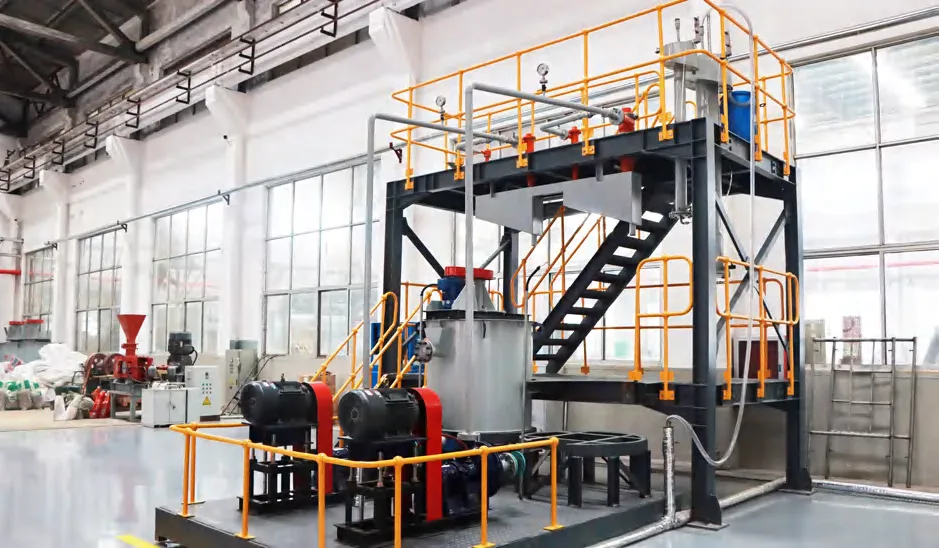
Copper Processing Plant Cost: What Moves the Budget
A copper processing plant cost is not a price list item; it is the sum of geology, flowsheet and site decisions made before you ever pour concrete.
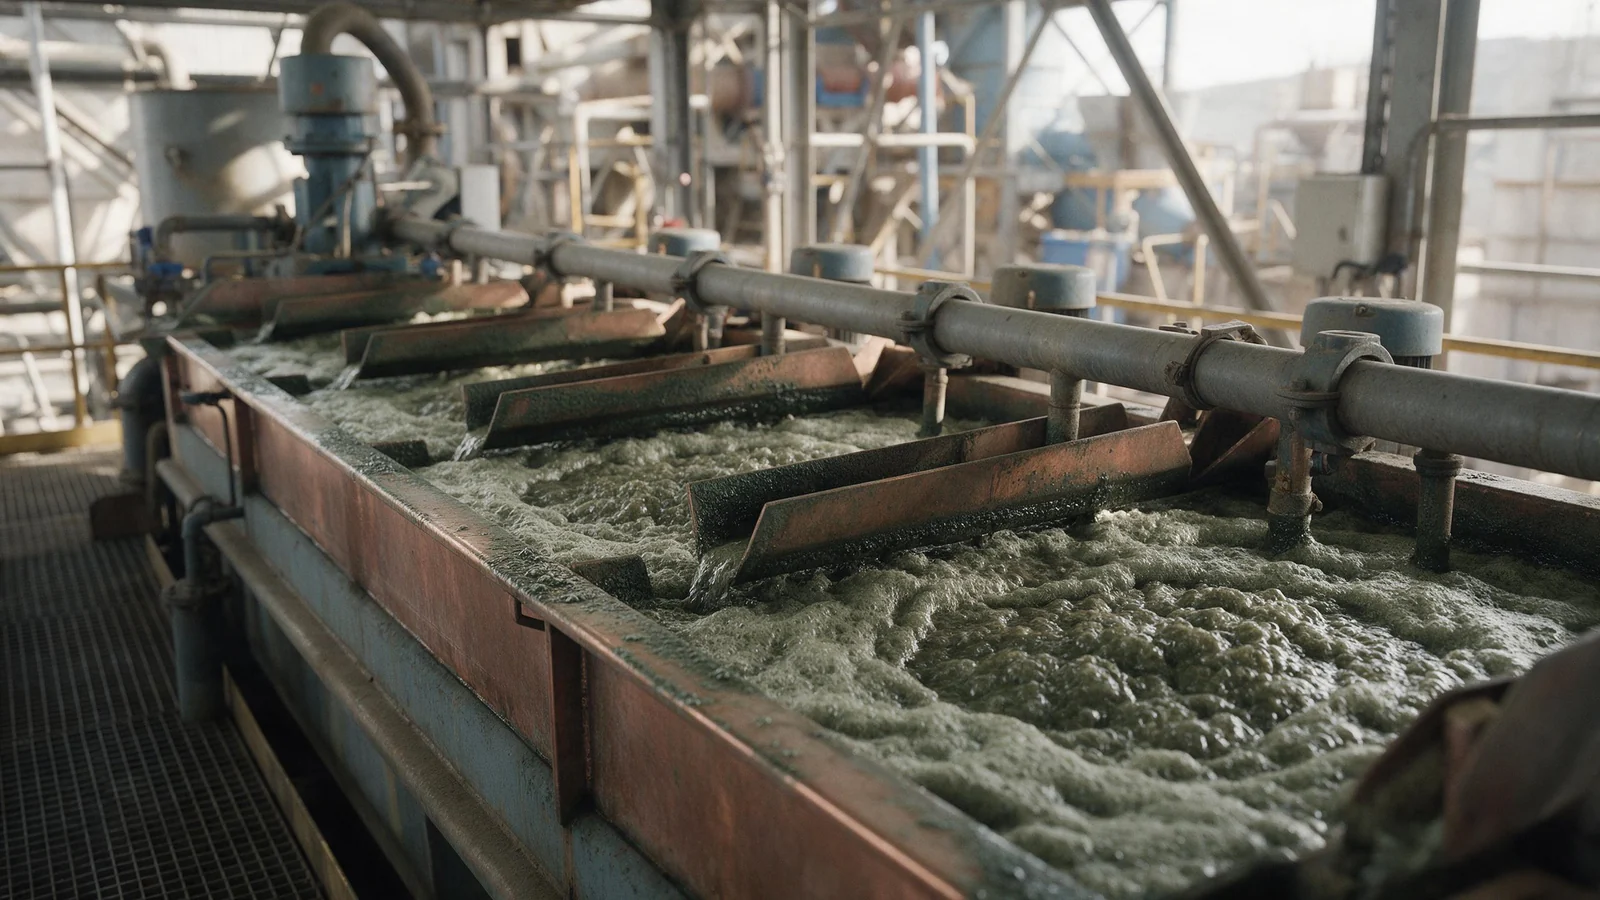
Say a mine owner asks what drives a copper processing plant cost. It isn't a sticker price. It's the sum of ore hardness, grind target, flotation circuit configuration, dewatering, tailings, power, water and distance. You don't buy a plant. You design one. Copper concentrators are custom machines, and every one of those variables changes the capital estimate.
What Actually Drives a Copper Concentrator's Capital Cost
Ore grade and hardness are the first two. A high grade ore lets you float less mass for the same metal output, so the plant is smaller. A low grade ore pushes tonnage up and the plant becomes a bulk materials handling exercise as much as a chemical one. Hardness matters because it sets the grinding duty. The Bond work index is a measured grindability parameter. A high value means more installed mill power, bigger motors, more grinding media and often a second stage of milling before flotation.
Grind size then fixes the whole downstream. If copper minerals liberate at a coarse size, you'll pay less than if they need very fine grinding. Finer grinding means more cyclone capacity, more regrind mills and more power. Flotation follows. A simple copper sulphide ore with fast kinetics can run a roughing and two cleaning stages. A complex ore with locked particles and slow floating copper needs more cell volume, longer residence time and a regrind circuit on the rougher concentrate. That regrind is not optional; it's often the difference between a saleable concentrate and a middling pile.
Dewatering and tailings are the quiet budget eaters. Copper concentrate needs thickening and filtering before shipping. Tailings need storage, water recovery and sometimes paste or filtered disposal. A remote site with poor water supply will add desalination, pipelines and camp costs. Power is another large line item. High altitude or off grid sites often need their own generation. All of these are decided by ore characterisation, not by a brochure.
How Plant Capacity and Process Route Change the Budget
Throughput sets the frame. A small plant is a set of standard machines on steel skids. A large plant needs a proper concrete mill building, a bigger crushing station and a tailings system that can handle the flow. But scale does not drop the cost per tonne in a straight line. Remote sites lose economy of scale quickly. Transporting a 100 tonne mill shell up a mountain costs more than the mill shell in some places. So a small plant near a port can be cheaper per tonne than a large plant two days from the nearest road.
Process route is the next fork. A concentrator producing a flotation concentrate stops at dewatering and loadout. If you add a leach or SX/EW circuit, you're buying tank farms, solvent extraction settlers and electrowinning cells. A smelter is a different animal entirely, with acid plants and gas handling. Most copper oxide projects choose heap leach and SX/EW, while sulphide projects go flotation. The route is dictated by mineralogy, and the capital cost moves by multiples between routes.
CAPEX vs OPEX: Where the Money Goes Over the Plant Life
Capital cost categories are straightforward: process equipment, civils and concrete, electrical and instrumentation, utilities like air and water, and contingency. Contingency is not a fudge factor; it's the honest admission that early estimates miss underground conditions, vendor lead times and bad weather. Operating cost categories are power, reagents, grinding media, labour and maintenance. Grinding media and liners wear out continuously. Reagents for flotation, especially collectors and frothers, scale with tonnage and ore chemistry.
The design stage locks in most of the life of mine cost. You can't change a mill's power draw once it's bolted down. You can't move a tailings dam easily. A testwork driven flowsheet may cost more in engineering hours up front, but it avoids overbuilt mills and underfed flotation banks that eat cash for twenty years. That is why prefeasibility testwork is not a cost; it's a saving.
The Cost Role of Ore Testing and Flowsheet Development
Before any estimate means anything, you need a sample that actually represents the orebody. Composite sampling is the usual starting point. The reference method for collecting ore samples is stopped belt sampling, as stated in ISO 8685:1992. A grab sample from a stockpile is almost useless for design. You need mineralogical analysis, chemical assays, density and Bond work index testing. Metallurgical laboratories run these daily. Xinhai's mining research institute operates a CNAS-accredited laboratory, covers more than 70 ore types and performs around 5,000 element analyses per month.
Open circuit flotation tests are good for comparing reagents. Locked cycle tests are what you need for a plant design. They recycle middlings and simulate a full circuit. The locked cycle result gives a realistic recovery and concentrate grade, and that feeds the mass balance and the equipment sizing. Without locked cycle data, you're guessing at flotation residence time and cleaning capacity. Guess wrong and you'll either overpay for cell volume or underbuild and lose recovery.
A flowsheet is not a collection of unit operations. It is the financial model of the plant. Every recycle stream, every regrind step, every wash water line appears in the operating cost. That is why testwork is the first real cost estimate tool, not a budget spreadsheet.
Equipment Selection and How It Affects the Estimate
Crushing and grinding are the power hogs. A primary jaw or gyratory crusher sets the top size. Then a SAG mill or a ball mill circuit grinds to flotation feed size. The mill size is driven by the Bond work index and the throughput. A harder ore may need a variable speed drive and a larger motor, both of which add capital and installed power. Flotation cell sizing follows from laboratory kinetics. More cells or deeper cells change the tank farm layout and the air blower duty.
Regrind is the hidden step. A rougher concentrate often needs a small ball mill or stirred mill before cleaning. That mill is not just another machine; it adds a cyclone, a pump, a sump and a lot of piping. Dewatering then thickens the concentrate, and a filter presses the water out for transport. Tailings pumping and storage complete the loop. The table below shows how a measurement becomes an estimate line.
| What you measure | What it changes | Why it hits the estimate |
|---|---|---|
| Bond work index, kWh/t | Mill motor size, grinding media charge | Harder ore may need two stage grinding or a larger mill |
| Liberation grind size, P80 | Cyclone and regrind mill selection | Finer targets multiply grinding energy and equipment count |
| Locked cycle flotation recovery | Number of rougher, cleaner and scavenger cells | Slow kinetics require more residence time and tank volume |
| Concentrate moisture | Thickener diameter and filter area | High moisture concentrate needs more dewatering capital |
| Tailings rheology | Tailings storage design and water recovery | Clay rich tails change dam construction and closure obligations |
A concentrator only plant stops at dewatering and loadout. The incremental cost of regrind, concentrate dewatering and tailings storage often dominates remote site budgets. Do not compare a bare flotation circuit quote from one supplier with a full EPC scope from another. They are not the same plant.
Shandong Xinhai Mining Group Co., Ltd., founded in 1997, reports more than 600 Mine EPC+M+O projects, according to the company's published figures. Its project list includes a copper flotation project in Kazakhstan with a yield of 3.50%, a Cu grade of 16.23% and a recovery of 66.23%, and a 1,500 t/d copper concentrator design in Pakistan. These numbers are specific to those ores. They are not transferable to yours.
Location, Infrastructure and Regulatory Costs
Location is not a line item; it's a multiplier. A plant near grid power, sealed roads and a port will cost far less for the same flowsheet than one three hundred kilometres from the nearest substation. You'll need a power line, a water borefield, an access road, a camp, and probably a fuel farm. At altitude, engine and motor derating adds cost. In a seismically active zone, civil works get heavier. Modular construction offers one way to control remote site labour, but it doesn't remove the need for local civils and foundation work.
At a remote site you'll need to ask:
- Is there a power line nearby, or do you build your own?
- Can you get water rights, and what treatment is required?
- Who owns the access road, and will it take the loaded haul trucks?
Permits and tailings management are the slowest costs. Environmental approvals can take longer than engineering. Water discharge limits may force you to install a zero discharge tailings system. That changes the tailings thickener and pump selection. The US Geological Survey reported that in 2024 net import reliance for copper in the United States was 45% (USGS Mineral Commodity Summaries 2025). That import share doesn't set your plant cost, but it does shape project economics and the pressure to build domestic capacity.
How to Get a Defensible Cost Estimate for Your Ore
Generic per tonne figures mislead because they average out the very things that decide your cost: grade, hardness, liberation size and location. A bankable feasibility estimate starts with a measured sample, a mass balance and vendor quotes for major equipment. Then you add civils, electrical, piping and a contingency that reflects the study stage. If you skip testwork and ask for a budget number, any supplier will give you one. It just won't mean anything.
When you involve an EPC contractor, ask for an estimate that separates direct equipment, bulks, civils and indirect costs. Ask for a quotation checklist like the table below. A complete copper plant quotation must itemise scope boundaries. If the number doesn't say what is excluded, it is not a quotation; it is a conversation starter.
| Quotation line | What to look for |
|---|---|
| Equipment list | Each crusher, mill, flotation cell, pump and tank with duty point |
| Drive and motor sizes | Installed power for each machine, not just the mechanical package |
| Wear materials | Liner and impeller metallurgy, expected life basis |
| Automation scope | Instrument list, control system level and motor control centre |
| Spares | Commissioning spares and recommended two year operating stock |
| Shipping and installation | Incoterms, site unloading, craneage and commissioning support |
| Exclusions | Power line, water supply, tailings dam, camp and permits |
Shandong Xinhai Mining Group Co., Ltd.'s mine design institute holds a Class B metallurgical industry design qualification and designs to JORC, NI 43-101, VALMIN, GB, Eurocodes, US and Australian standards. That qualification is one of the things a bank or partner will ask about. But no standard replaces your own testwork. Test the ore, size the machines, then compare quotes line by line. That is the only defensible path to a copper processing plant cost.
For a small or low-grade deposit, the small-scale copper processing plant page sets out the usual capacity bands, the flowsheet options and the ore data needed before anyone can quote.
Frequently asked questions
How much does it cost to build a copper processing plant?
There is no fixed number. Capacity, ore hardness, grind size, flotation stages, tailings storage and remoteness change the figure by multiples. Ask for an itemised estimate after testwork, not a budget quote. The sections above list the drivers that move the total.
Is copper mining profitable?
It can be, but profitability depends on margin, not tonnage. The three big swings are head grade, recovery and operating cost. Power, reagents and grinding media dominate operating cost. Capital cost per annual tonne is the other side. A plant built with an oversized mill or the wrong flowsheet may never recover its capital. Test first, then judge.
How much is 1 ton of copper ore worth?
It depends on grade and recovery. A tonne of low grade ore contains only a small amount of copper, and you won't recover all of it. Payable metal after milling, smelting and refining is the only thing that matters. Transport, treatment charges and moisture also cut the net value. Without a grade and recovery figure, any number is guesswork.
Can the US produce enough copper for itself?
Not at current demand. The US Geological Survey reported that in 2024 net import reliance for copper as a percentage of apparent consumption was 45%. Domestic mine production and refining meet part of the need, but just under half comes from imports. So no, not unless production expands or demand shifts.